Applications
The Liquimech Floating Water Intake System is ideal for:
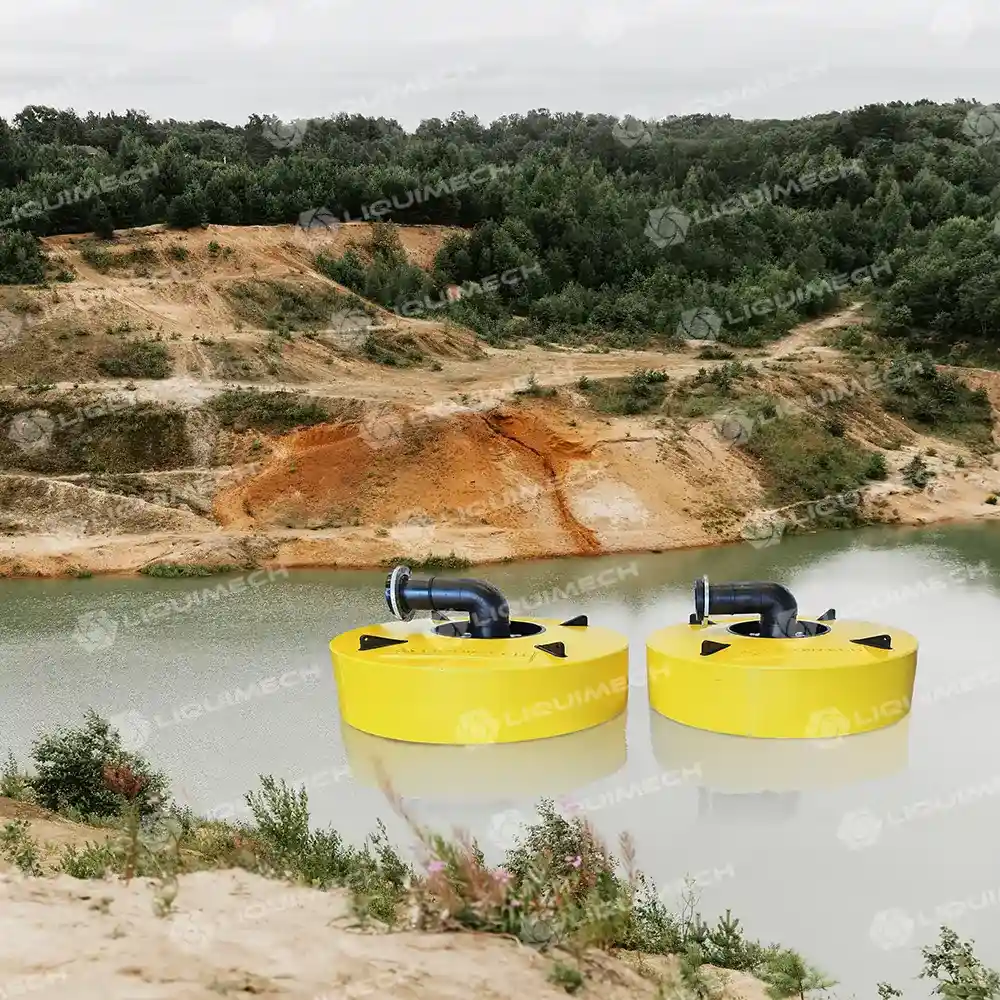
- Mine dewatering
- Tailings Water Recovery
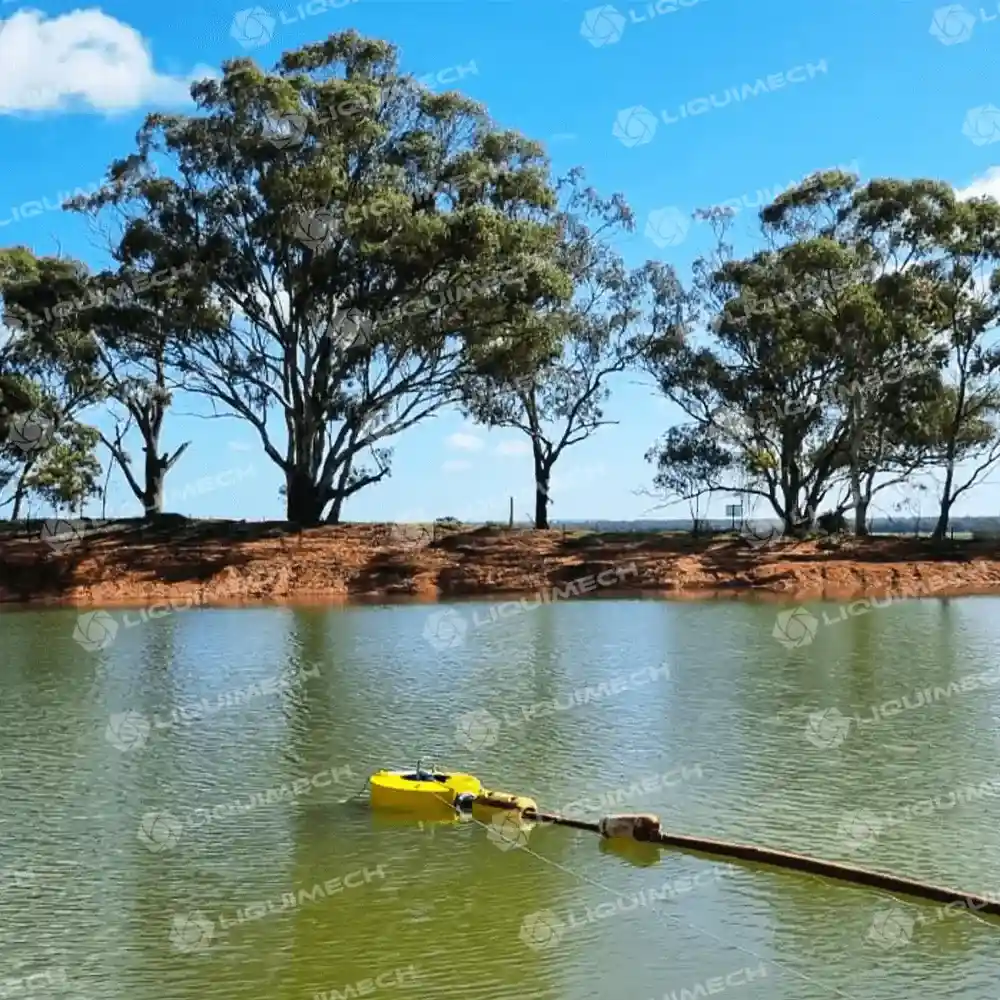
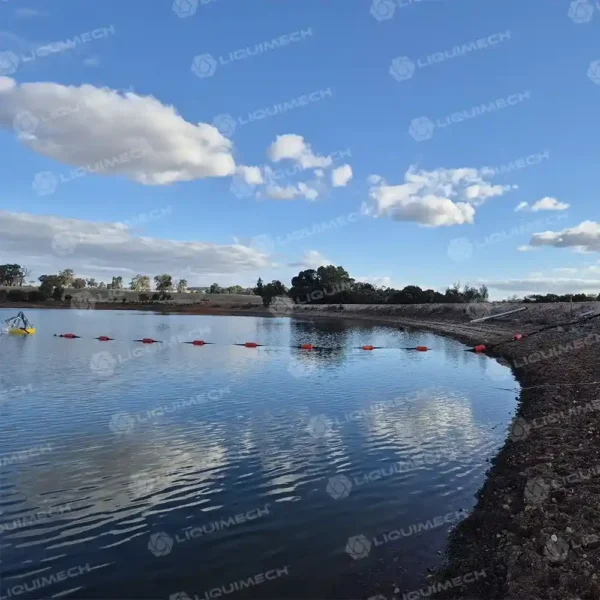
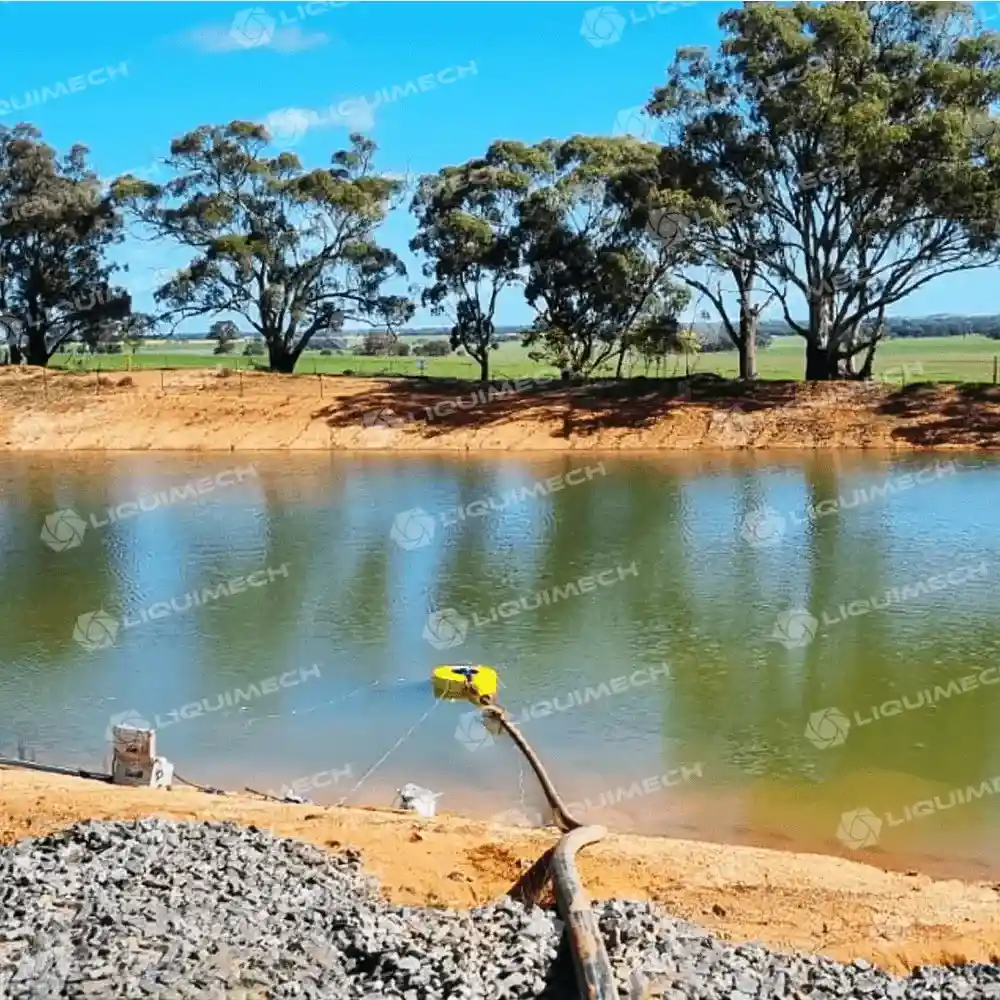
- Dam and Pond Water Extraction
- Water transfer
- Industrial pumping
- Civil Construction Projects
- Irrigation systems
- Farm dams
- Livestock Watering
- Reservoirs
- Water storage ponds
- Freshwater supply
- Process water
- Emergency water supply
- Fire Fighting Water Supply
- Environmental water management
- Industrial Water Management
Industries We Serve
Mining
Protect dewatering pumps from sediment and cavitation while improving operational reliability.
Agriculture
Maintain consistent irrigation water supply from shallow dams, rivers, and reservoirs.
Civil Construction
Reliable temporary and permanent water transfer systems for infrastructure projects.
Water Authorities
Improve water quality entering pumping systems while reducing maintenance.
Industrial Operations
Reliable water transfer for processing plants, quarries, and heavy industry.
Complete Water Transfer Solutions
A pump intake is only one part of a reliable water transfer system.
Liquimech delivers complete engineered solutions from concept through commissioning.
Our experienced engineering team can supply:
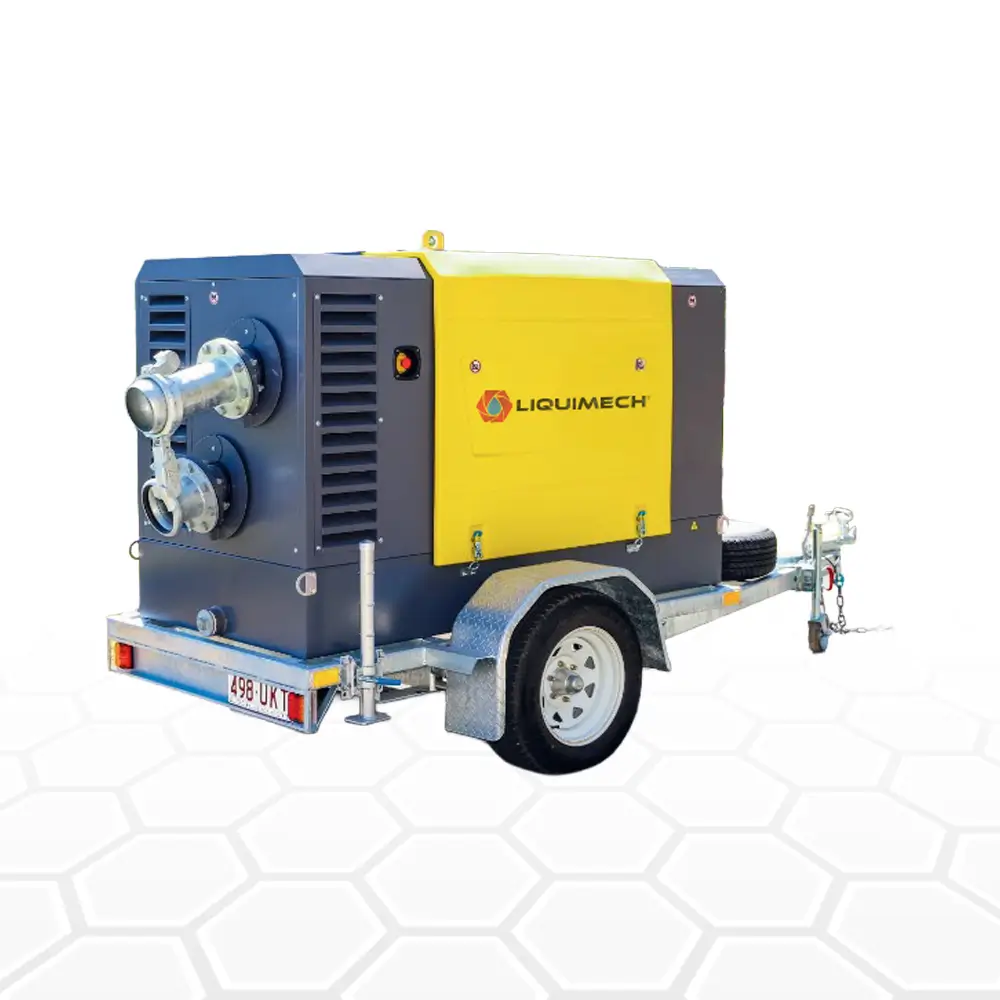
- Land-based pumps
- Amphibious pumps
- Submersible pumps
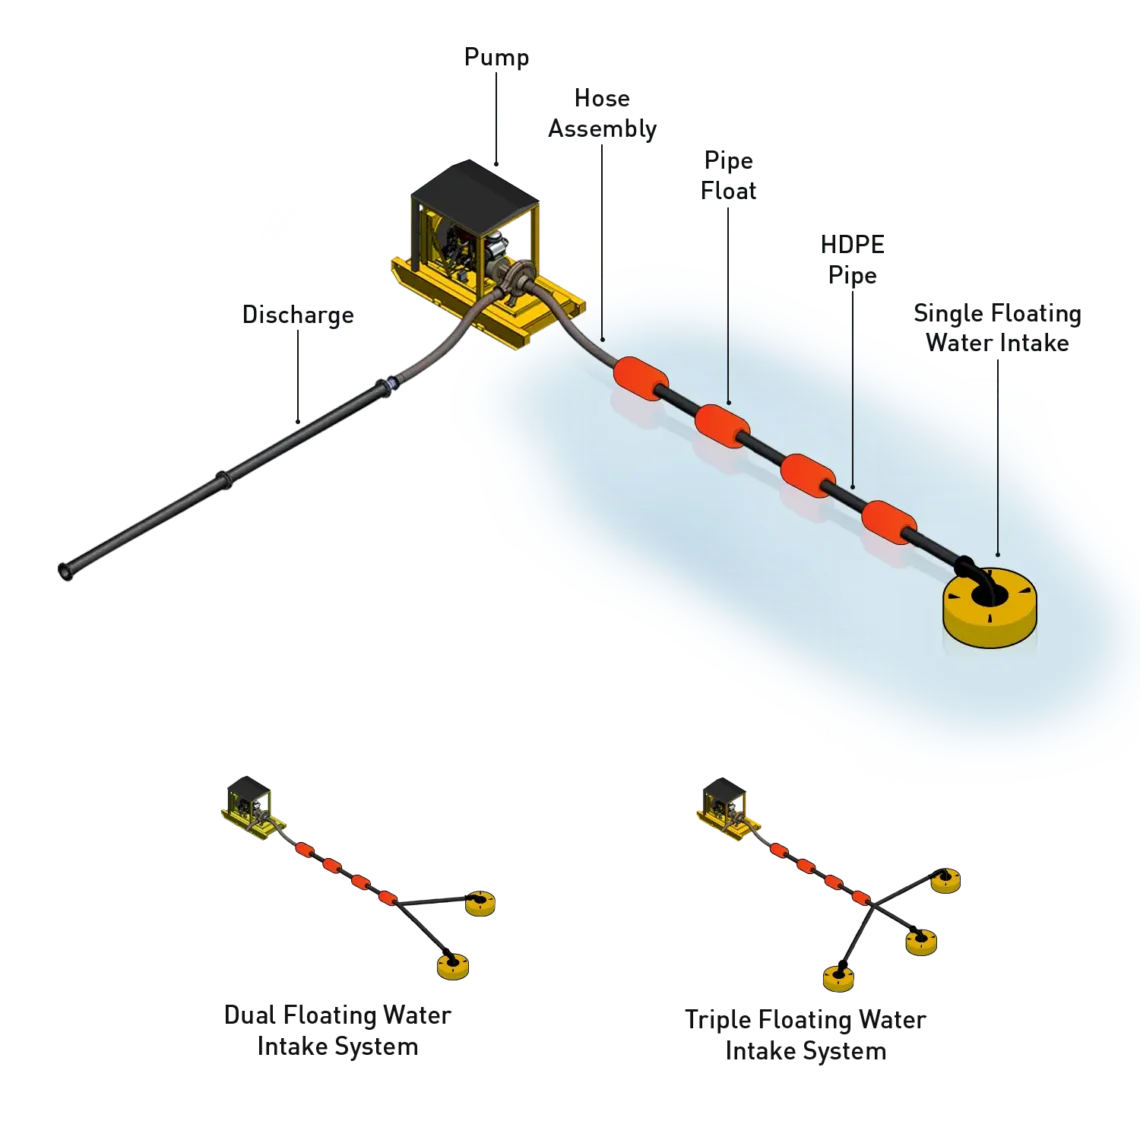
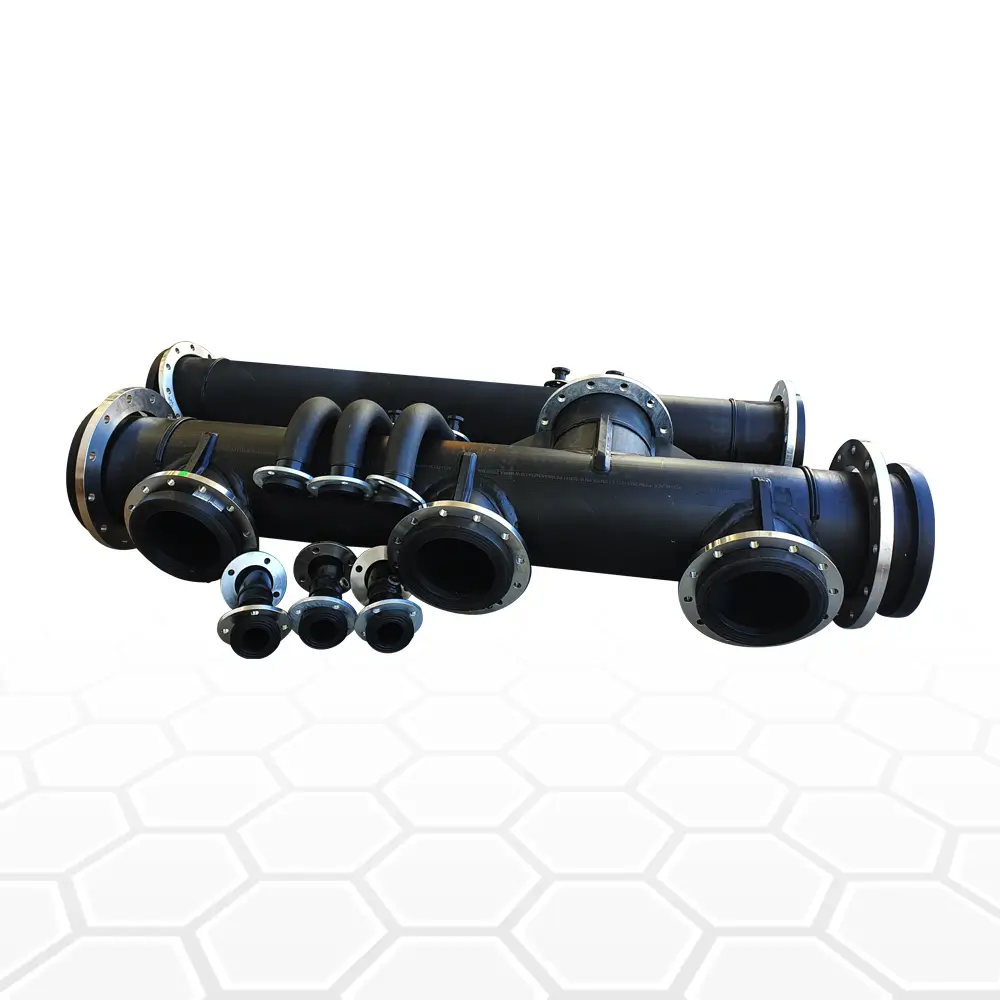
- HDPE pipe systems
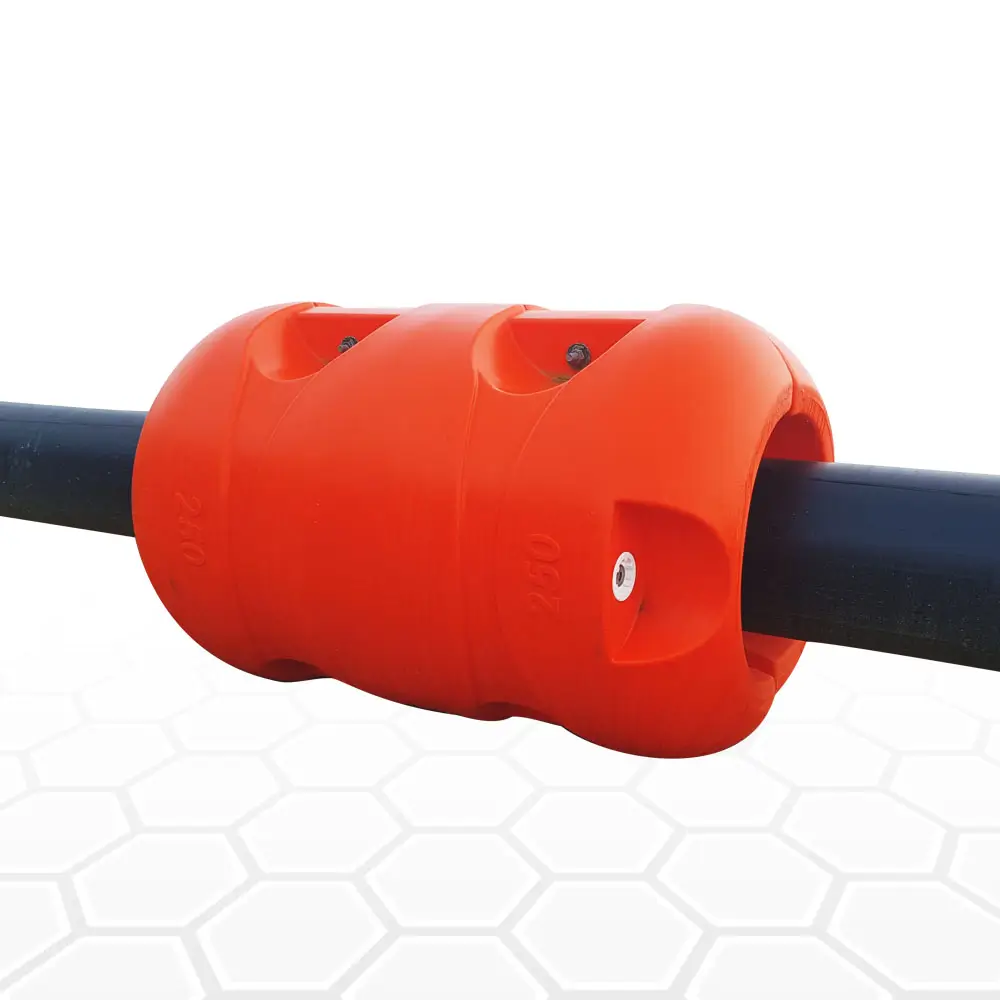
- Pipe floats
- Pipe spools
- Reducers
- Valves
- Hoses
- Custom pumping packages
Reliable Floating Water Intake for Mine Dewatering Applications
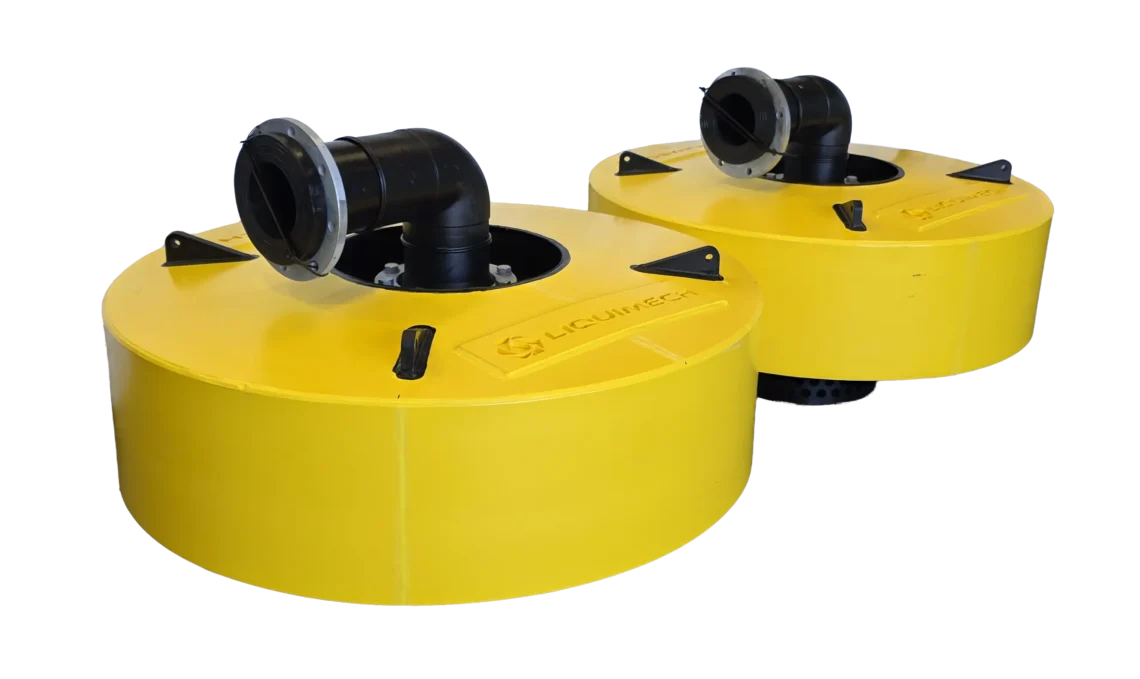
Managing water levels in dams, mine pits, tailings facilities, and process water ponds can be challenging. Liquimech Floating Suctions provide a reliable floating water intake solution designed to draw cleaner water while protecting pumping equipment from common causes of failure.
How Do Liquimech Floating Suctions Help?
- Improve pump performance and operational efficiency
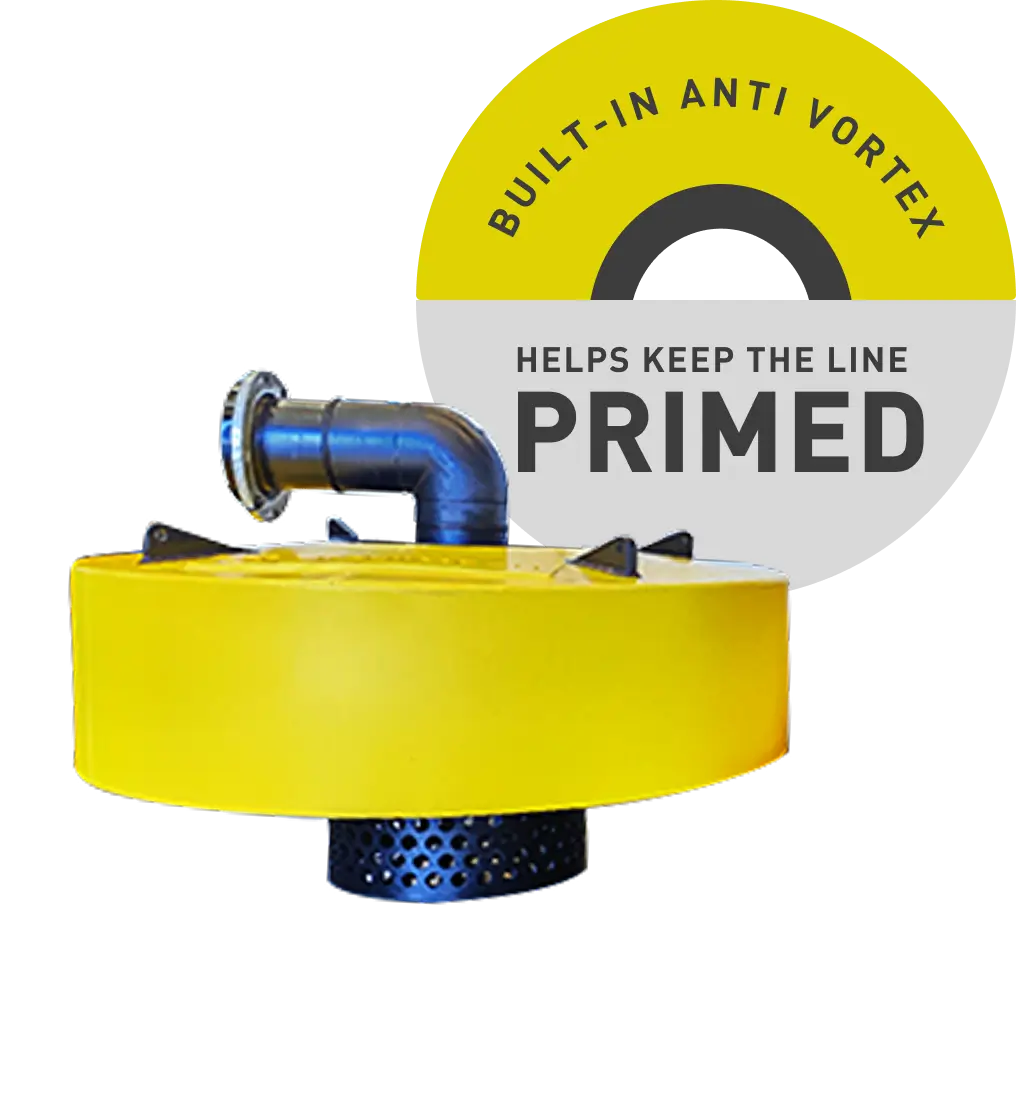
- Reduce vortexing and cavitation that can damage pumps
- Minimise sediment and tailings ingestion
- Support effective mine dewatering and water transfer operations
- Lower maintenance requirements and operating costs
- Adapt to changing water levels for consistent pump performance
Fire Fighting & Emergency Water Supply
During emergency response situations, every minute counts. Firefighting crews often bypass shallow water sources in search of deeper refill points, increasing travel time and reducing water availability on site.
How Do Liquimech Floating Suctions Help?
- Enable water extraction from shallow water sources, with operation in water depths as low as 180 mm*
- Provide a reliable water supply for firefighting and emergency response applications
- Compatible with trailer-mounted pumps and portable pumping systems
- Lightweight design for easy handling, deployment, and retrieval
- Ideal for rural, regional, and remote Australia
*Application suitability depends on pump configuration and site conditions.
Every component is selected to work together as one integrated system, reducing installation time, improving reliability, and lowering total operating costs.
Agriculture & Irrigation
Efficient water management is critical for agricultural productivity. Liquimech Floating Suction Valve Systems help deliver cleaner water from dams, ponds, and storage reservoirs while protecting pumps from air entrainment and sediment ingestion.
How Do Liquimech Floating Suction Valve Systems Help?
- Minimise vortexing and air ingestion
- Reduce cavitation and pump wear
- Improve pump reliability and performance
- Deliver cleaner water for irrigation and water transfer applications
- Suitable for livestock watering, horticulture, viticulture, and broadacre farming
- Low-intake design helps minimise disturbance to aquatic environments
Frequently Asked Questions
What is a Floating Water Intake?
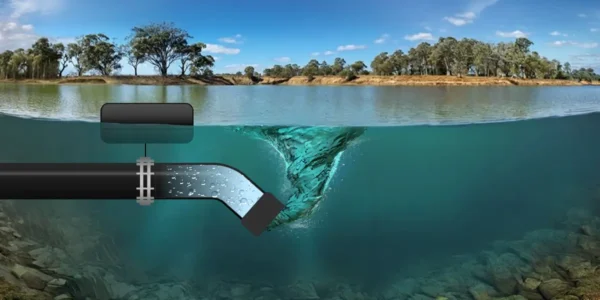
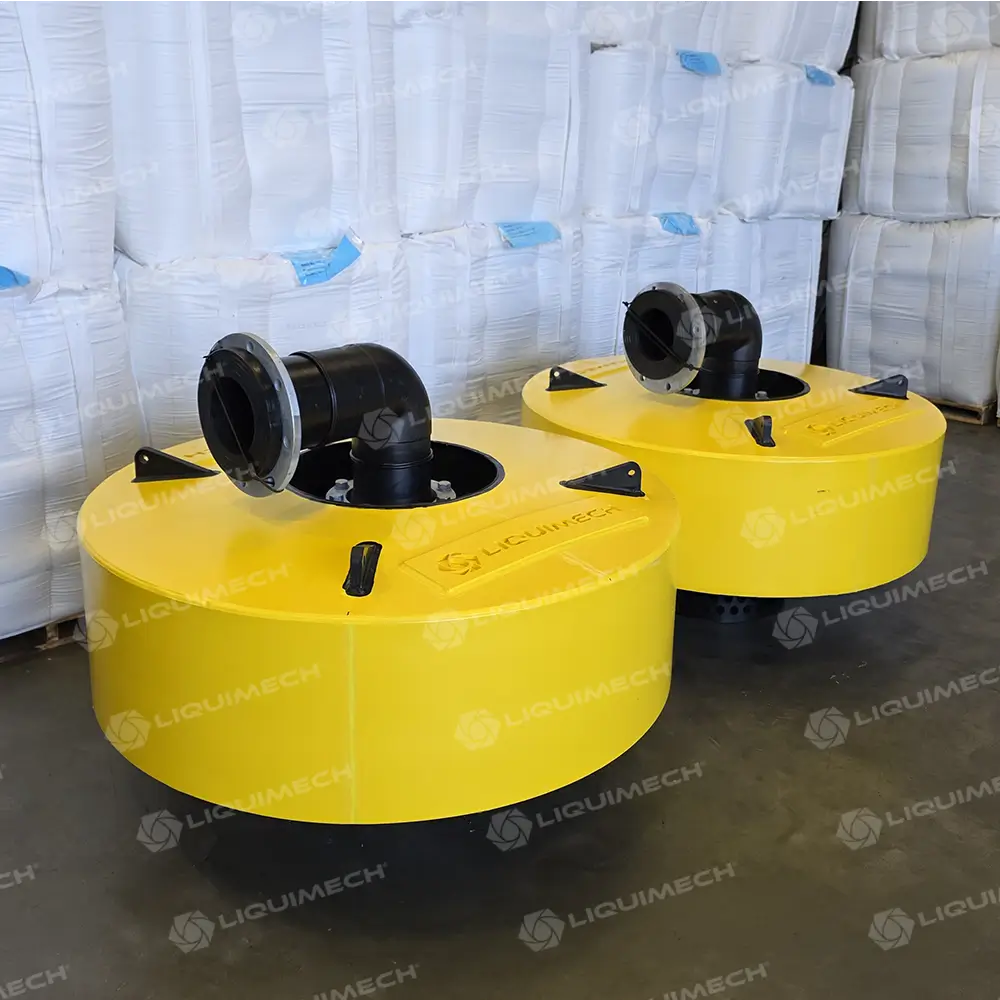
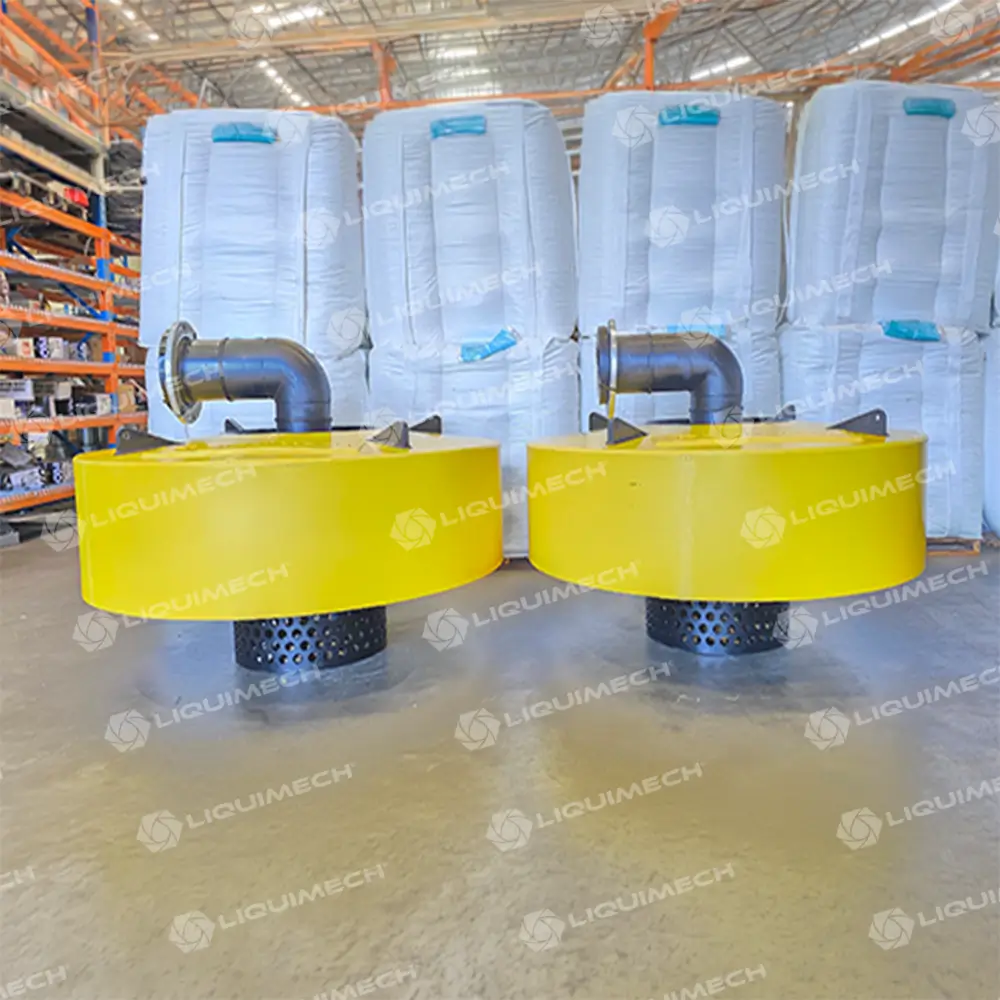
A Floating Water Intake is a buoyant intake system that keeps the pump suction at the optimal operating depth below the water surface. It helps reduce sediment ingestion, minimise vortexing, and improve pump reliability.
How does Anti-Vortex Technology work?
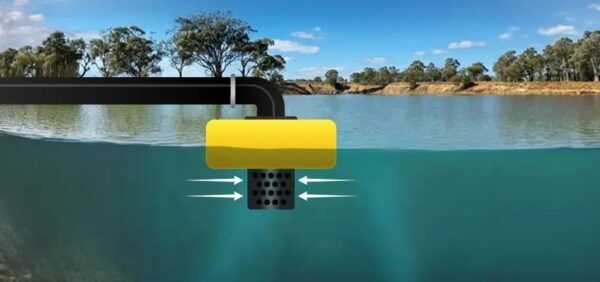
Liquimech’s water intake design distributes water evenly around the intake, slowing water velocity and helping reduce vortex formation, air entrainment, and cavitation before water reaches the pump.
Where can it be used?
The system is suitable for mining, dewatering, irrigation, dams, ponds, reservoirs, industrial water transfer, civil construction, and water management projects.
What is a Floating Pump Intake?
A Floating Pump Intake is designed to protect pumps by reducing the intake of sediment, debris, and air, helping extend pump life while improving pumping efficiency.
How do I prevent my pump from sucking sludge?
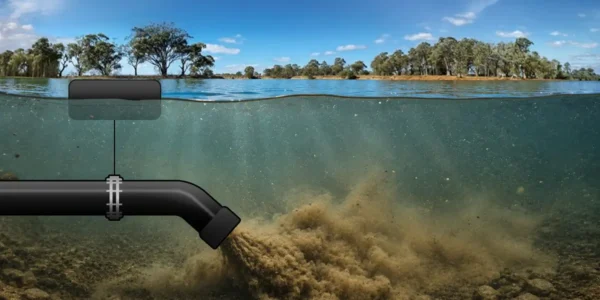
To prevent a pump from drawing in sludge, avoid placing the suction intake directly on the bottom of the dam, pond, or sump, where sediment naturally accumulates. Instead, use a Floating Intake for Pump that suspends the intake below the water surface while keeping it clear of sludge and settled material.
This approach helps reduce sediment entering the system, protects impellers and seals from abrasive wear, and improves the efficiency and reliability of your Floating Suction Valve Systems, particularly in mining, dewatering, irrigation, and water transfer applications.
How do you pump water without sediment?
The most effective way to pump water without sediment is to position the suction intake below the water surface but above the bottom, where the water is typically cleaner. This helps reduce the amount of sand, silt, mud, and debris entering the pump.
A Floating Water Intake System automatically maintains this optimal intake depth as water levels change. When combined with a Floating Suction Strainer and integrated anti-vortex technology, it helps minimise sediment pickup, reduce pump wear, and improve overall pumping reliability.
What is a Floating Suction Valve System?
A Floating Suction System is a floating intake assembly connected to the pump suction line. It automatically follows changing water levels while drawing cleaner water from beneath the surface.
Why Engineers Choose Liquimech?
Liquimech designs and manufactures engineered water management solutions trusted across Australia’s mining, industrial, agricultural, and infrastructure sectors. Our products are developed to solve real operational challenges; not simply supply equipment. Our Floating Suctions are designed to provide reliable water intake from shallow water sources while reducing vortexing, cavitation, and sediment ingestion. Ideal for mining, civil, industrial, agricultural, and emergency water transfer applications, they help maximise pump performance, minimise downtime, and extend equipment service life.
Every Floating Water Intake System is engineered to improve pump reliability, reduce maintenance, increase operational efficiency, and deliver long-term performance in demanding environments.
When reliability matters, engineers choose Liquimech.
Get a Quote on Your Floating Water Intake Today
Stop replacing damaged pump impellers and wasting time on site downtime caused by sludge ingestion. Talk to our engineering specialists today to get competitive pricing, detailed product specifications, or a custom quote tailored to your site requirements.